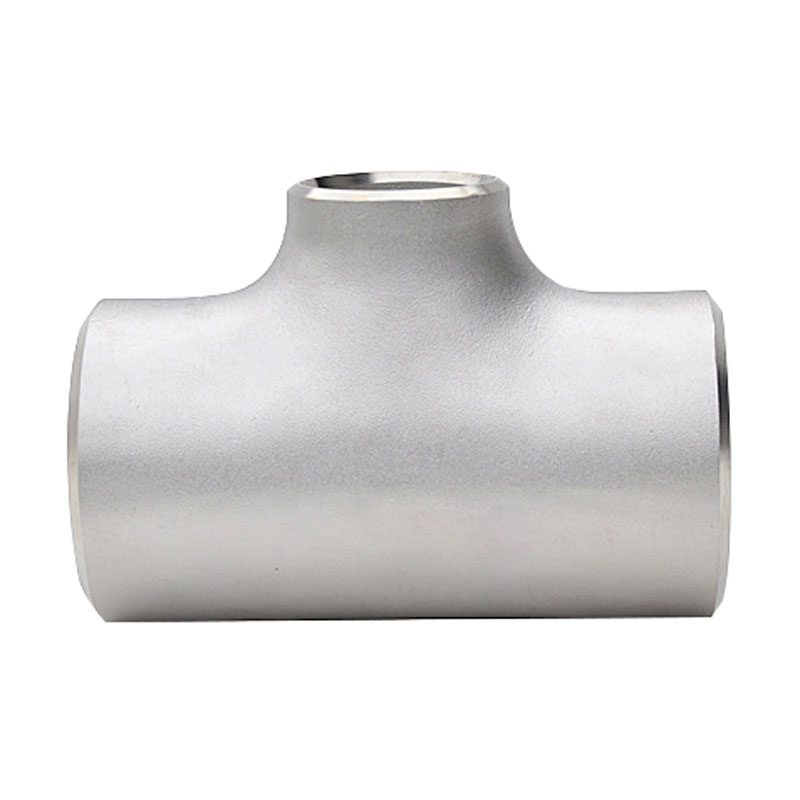
Seamless equal and reducing tees, DN15–DN2000, ASME B16.9.
| Size range | DN15–DN2000 |
|---|---|
| Types | Equal, reducing |
| Wall thickness | Sch5S–XXS, matched to pipe |
| Standards | ASME B16.9, GB/T 12459-2017, GB/T 13401-2017, SH/T 3408, DIN 2615, ISO 3419 |
| Ends | Butt weld, ASME B16.25 bevel |
| Testing | RT/UT, PMI and 1.5× hydrostatic on request |
A butt-weld tee is formed by hydraulic bulging or hot extrusion from seamless tube, so the branch is reinforced by thickened material rather than by a welded saddle. The result is a smooth bore, uniform wall at the junction and predictable pressure containment.
Hydraulic bulge forming for DN15–DN300 keeps ovality ≤1% and gives a well-rounded branch transition.
Larger sizes are hot formed or fabricated from two seamless halves and full-penetration welded, then stress relieved.
All three ends machined to ASME B16.25 bevels matched to the pipe schedule.
Reducing tees are marked with run × branch dimensions, e.g. DN100 × DN80.
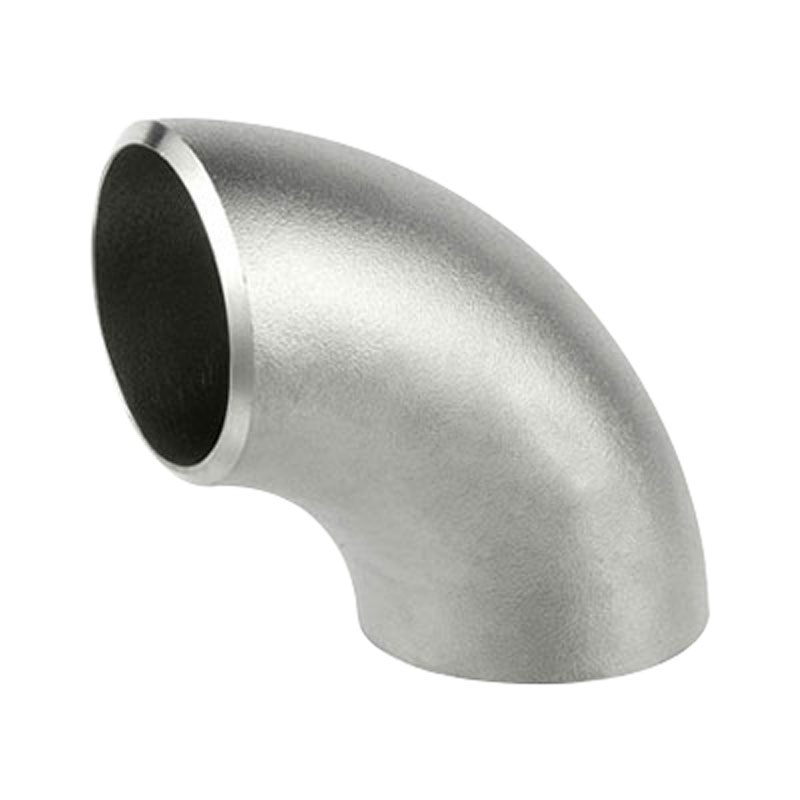
Seamless stamped 90° elbow, LR or SR, DN15–DN2000, to ASME B16.9 / GB/T 12459.
Specifications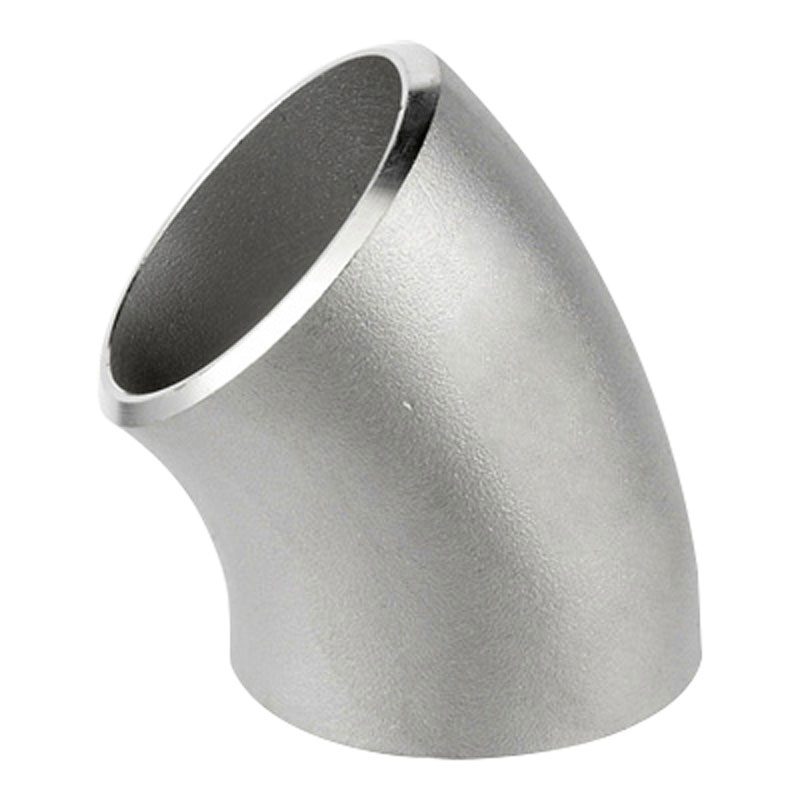
Seamless 45° elbow for gradual direction change with low pressure loss.
Specifications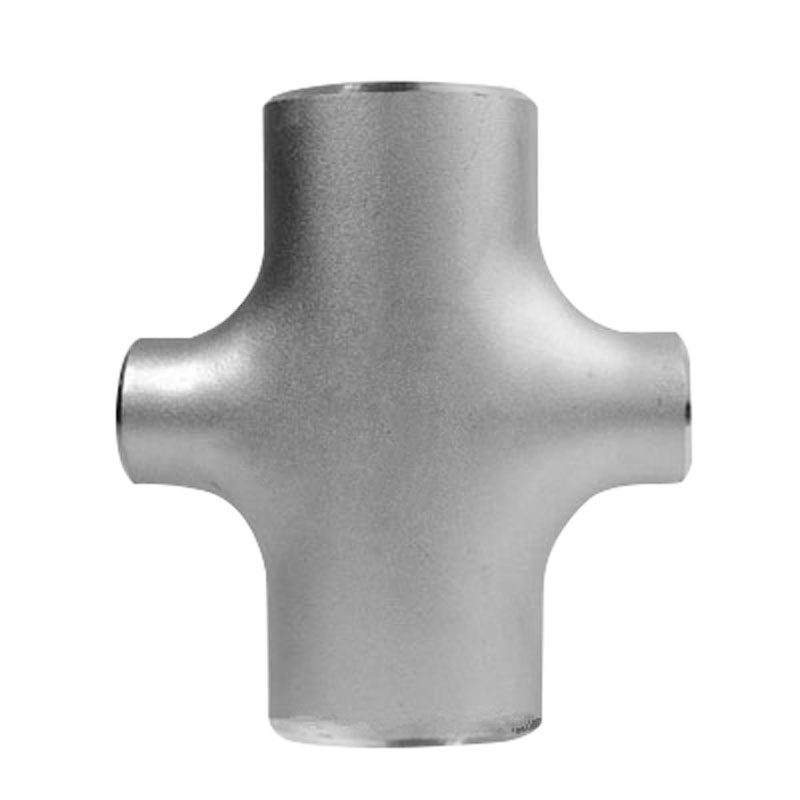
Four-way butt-weld cross, equal and reducing, seamless formed.
SpecificationsQuotes within one business day. Send grade, size, pressure class, face type and quantity — a drawing works better than a description.