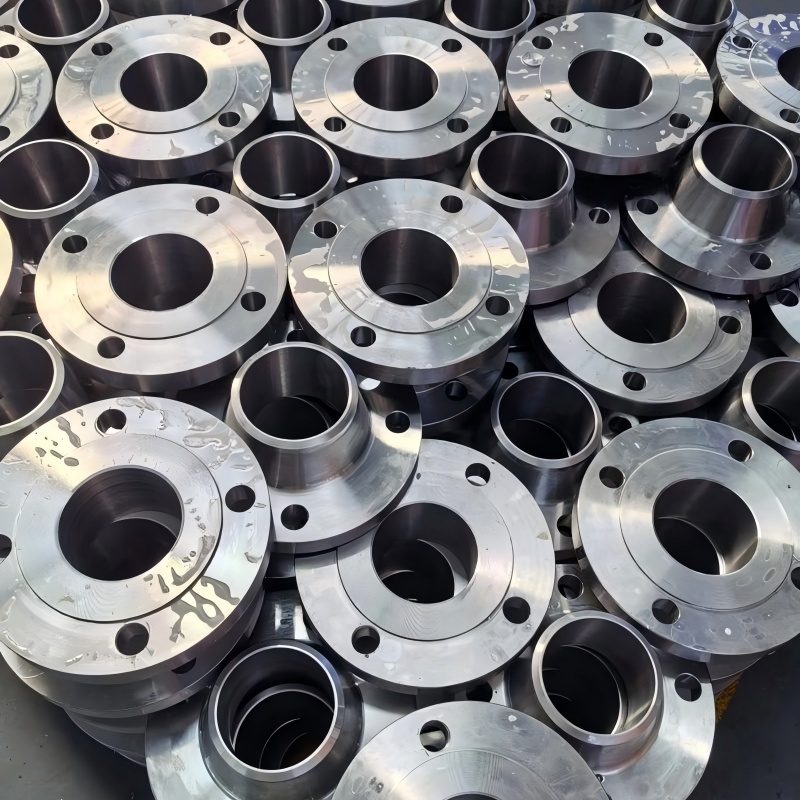
Long-hub WN flange butt-welded to pipe, for high pressure and cyclic service.
| Size range | DN15–DN2000 (NPS 1/2–80); larger sizes to drawing |
|---|---|
| Pressure class | PN2.5–PN400, Class 150–2500 |
| Standards | ASME B16.5, ASME B16.47, HG/T 20592-2009, HG/T 20615-2009, GB/T 9124.1-2019, EN 1092-1 |
| Face types | RF, FF, MFM, TG, RJ |
| Manufacture | Closed-die forging, normalised or solution annealed, CNC machined |
| Wall matching | Bore machined to the ordered schedule (Sch10S–XXS) |
A weld neck flange carries a tapered hub that transfers the pipe load into the flange body, so stress is spread over the butt weld instead of concentrated in a fillet. That is why it is the default choice for high pressure, elevated temperature and lines that cycle.
The bore is matched to the pipe inside diameter so there is no step at the weld root; the hub taper follows ASME B16.5 hub dimensions unless a project drawing overrides them.
Butt-weld ends are machined to ASME B16.25 bevels. Face finish is 125–250 AARH for RF and FF, and a smooth 63 AARH for ring-joint grooves.
Raised face (RF), flat face (FF), male-and-female (MFM), tongue-and-groove (TG) and ring joint (RJ) are all available; RF is standard.
For hydrogen, sour gas or steam above 400 °C, tell us the gasket type so the groove or face is machined to suit.
Heat number stamped on the rim, mapped to an EN 10204 3.1 certificate.
Dimensional report, PMI report and, where specified, hardness or impact results.
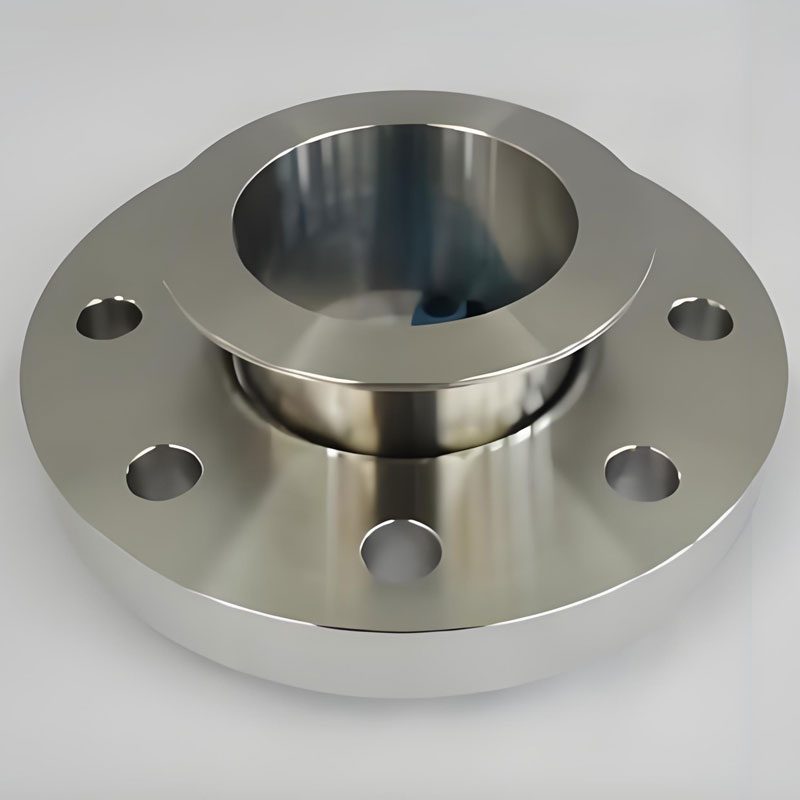
Rotating loose flange used with a stub end — easy bolt-hole alignment and cheap to replace.
Specifications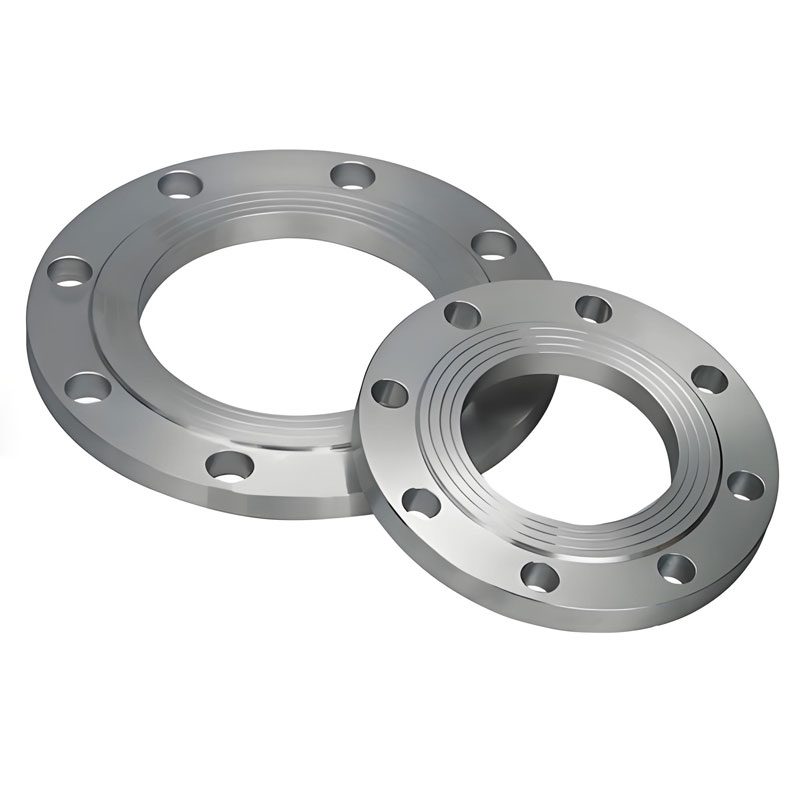
Plate flange slipped over the pipe and fillet-welded both sides — the economical standard flange.
Specifications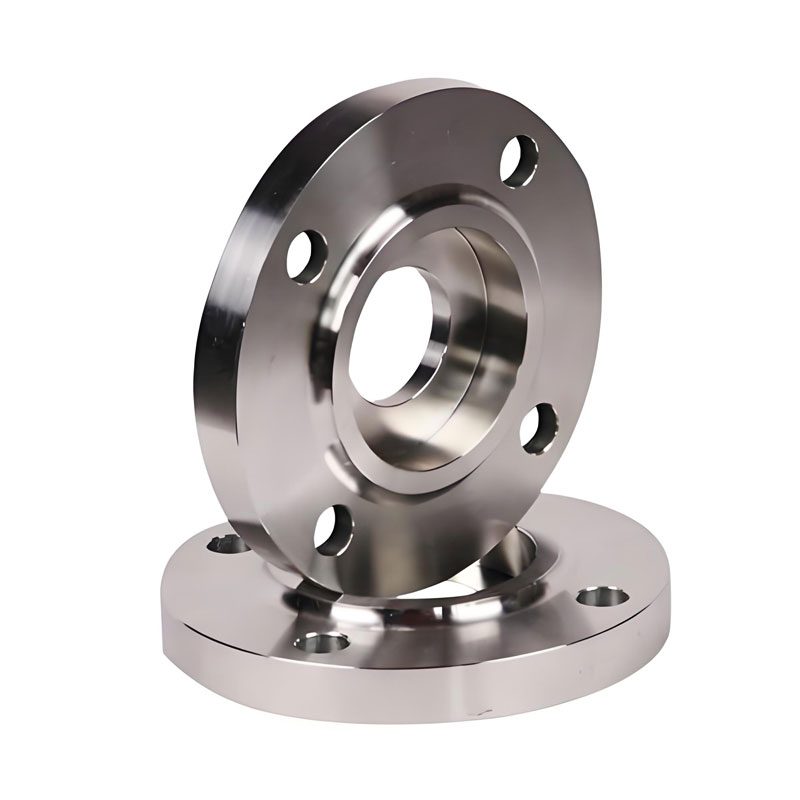
Small-bore socket weld flange, single external weld, DN6–DN100.
SpecificationsQuotes within one business day. Send grade, size, pressure class, face type and quantity — a drawing works better than a description.