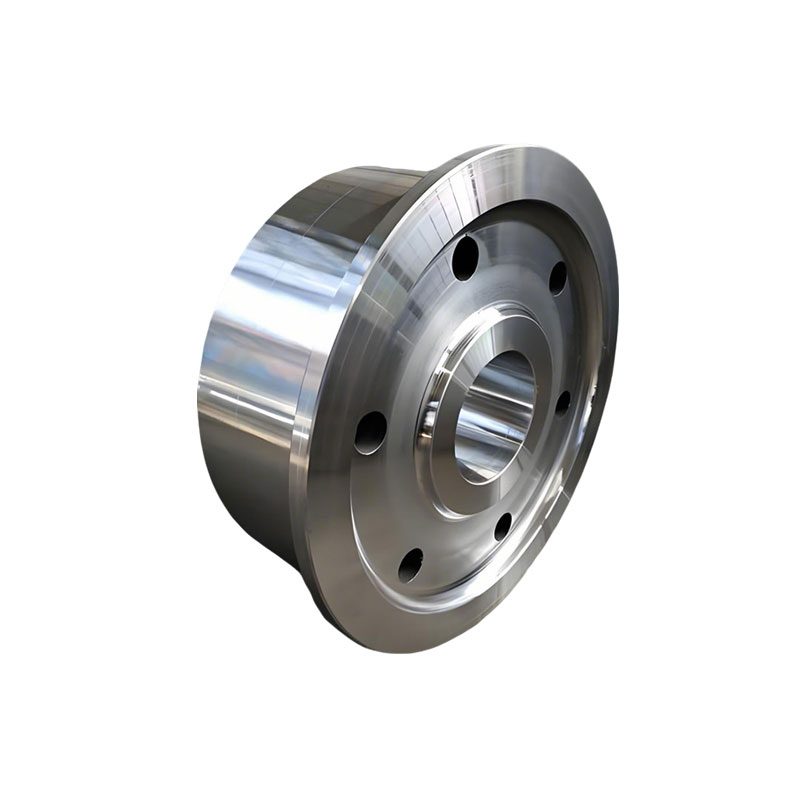
Non-standard forgings to drawing — complex profiles, thin walls, tight tolerances.
| Size range | A few millimetres to several metres, up to ~100 t per piece |
|---|---|
| Processes | Open-die, closed-die, isothermal forging, ring rolling |
| Tolerance | As-forged per GB/T 908-2019; machined to drawing |
| Standards | GB/T 908-2019, GB/T 6402, ASTM A388, ASTM A182, ASTM B564, RCC-M on request |
| Finishing | Normalising, annealing, Q+T, solution annealing, machining, passivation |
| Documentation | Material certificate, dimensional report, UT/PT/MT reports |
When the geometry does not exist in a catalogue, the part is forged to drawing. That covers curved support brackets, valve bodies, impeller blanks, thin-wall housings and anything else where a machined-from-solid part would waste material or lose grain flow.
Send a drawing or STEP file with the material, heat-treatment condition and inspection requirements. We return a forging drawing, a process route and a price.
Open-die, closed-die or isothermal forging is selected by geometry and lot size; machining, heat treatment and surface finishing can be included.
As-forged tolerance to GB/T 908-2019; machined features to your drawing, with position tolerances down to ±0.1 mm where specified.
UT, PT and MT are available; micro-focused dimensional inspection for thin-wall sections.
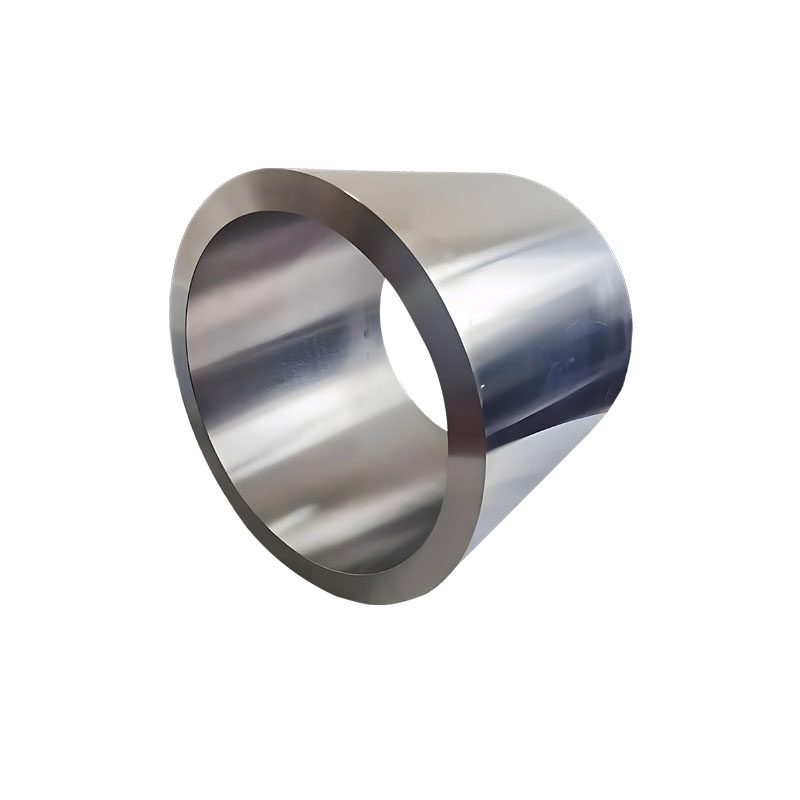
Seamless rolled rings up to 7.5 m outside diameter, IT7–IT9 tolerance.
Specifications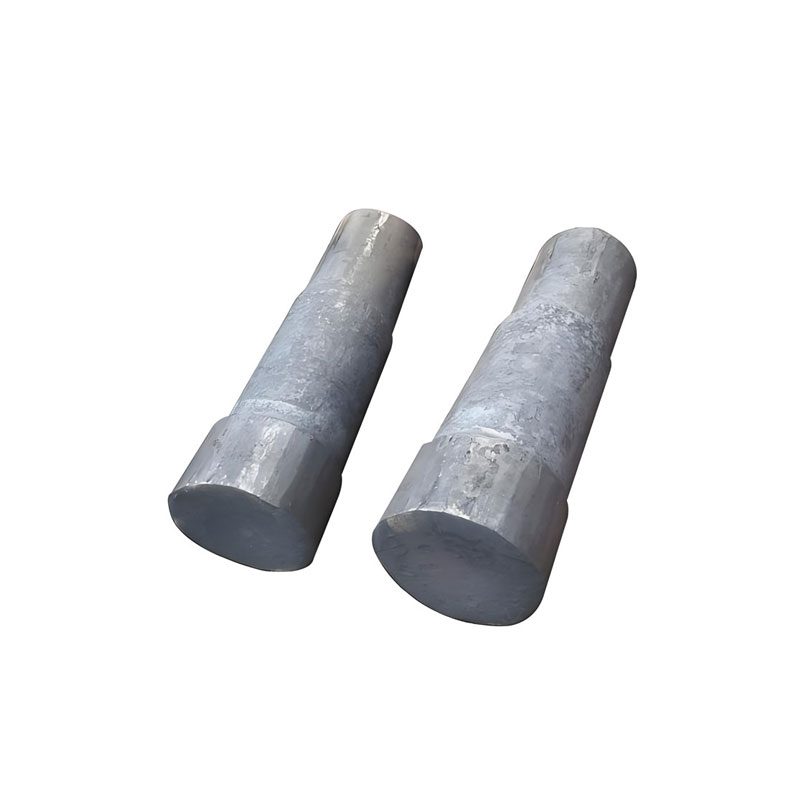
Forged round bar Φ80–Φ1200 mm, forging ratio ≥4:1, UT to GB/T 6402 or ASTM A388.
Specifications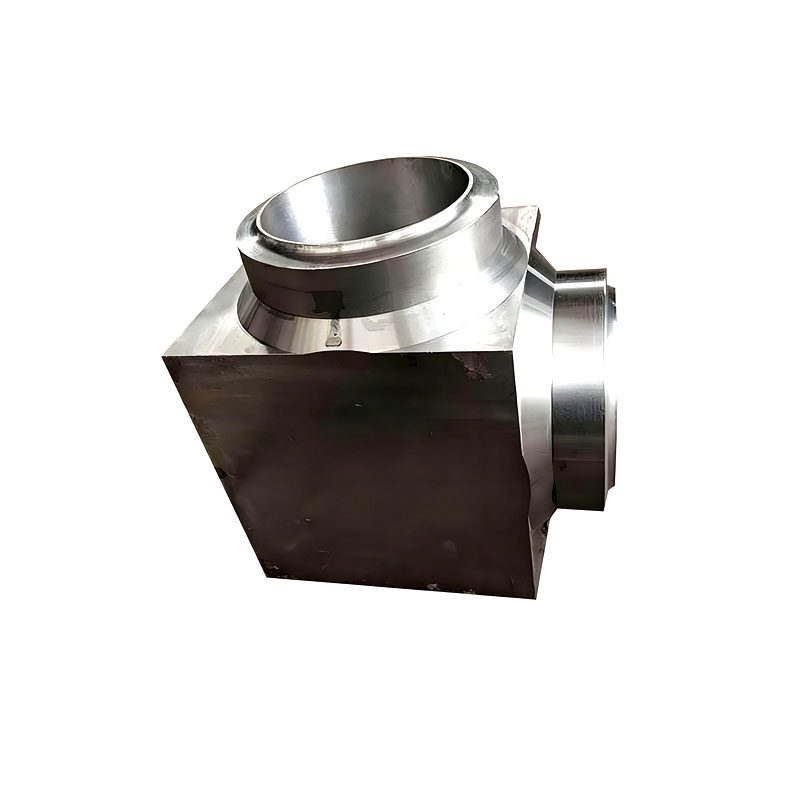
Forged square billet 40–1000 mm, dense core, for dies, tools and machined blocks.
SpecificationsQuotes within one business day. Send grade, size, pressure class, face type and quantity — a drawing works better than a description.